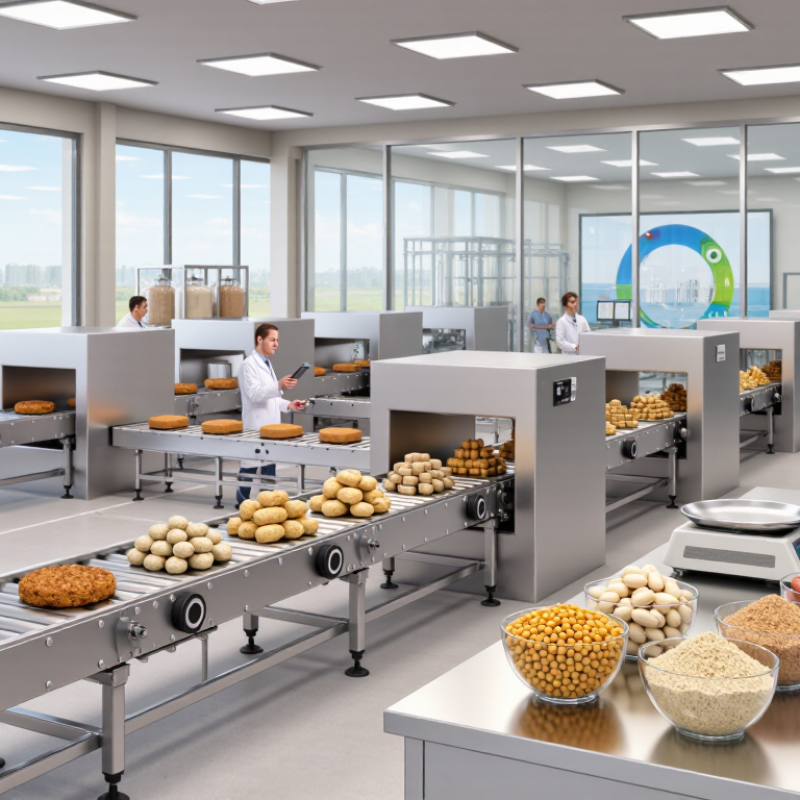
What Challenges Do Manufacturers Face With Plant Proteins?

Time:2026-09-23 Author:Liam
0%

Manufacturers are investing heavily in plant-based products, but growth does not remove practical production barriers. The Good Food Institute reported that U.S. retail sales of plant-based foods reached $8.1 billion in 2023. However, unit sales weakened in several categories. This gap matters. Consumers may try a pea-protein burger once, then reject it because of dryness, bitterness, or a rubbery bite.

So, what challenges do manufacturers face when using vegetal proteins? Ingredient functionality is one. Pea, soy, fava, and wheat proteins behave differently during hydration, heating, and extrusion. Their performance also changes between harvests. A factory may receive protein with a slightly different particle size or moisture level. That can alter viscosity, flavor release, and final texture. Small changes become expensive at industrial scale.

Professor David Julian McClements has identified the central problem clearly: “The major challenge is to create plant-based foods that have the same taste, texture, and nutritional profile as animal-based foods.” His observation reflects current industry evidence, including research reviewed by the Food and Agriculture Organization and market analysis from the Good Food Institute. Manufacturers must manage off-flavors, incomplete protein profiles, allergen controls, water use, and rising formulation costs. Nutrition claims also require careful verification. A product can be sustainable in one metric, yet weaker in another. The industry sometimes oversimplifies this point. Better products will come from measured testing, transparent labels, and recipes designed for real kitchens, not only laboratory demonstrations.

What Challenges Do Manufacturers Face With Plant Proteins?

Defining Plant Proteins and Their Role in Modern Manufacturing

What Challenges Do Manufacturers Face With Plant Proteins?

Defining Plant Proteins and Their Role in Modern Manufacturing

Plant proteins are concentrated nutrients extracted from peas, soy, lentils, beans, and grains. They can support muscle nutrition while reducing reliance on animal-based ingredients. In modern manufacturing, their role extends beyond protein content. They help create structure, moisture retention, emulsions, and satisfying textures in many foods.

Manufacturers often face inconsistent raw materials, earthy flavors, weak binding, and difficult hydration. Protein behavior can change with harvest conditions, processing methods, and storage time. Heat may improve safety but damage texture. Mixing speed also matters. A powder that disperses smoothly in a laboratory can form stubborn lumps on a busy production line. This gap requires careful pilot testing, sensory evaluation, and reliable quality records. Some formulations appear successful at first, yet become dry after several weeks. That result deserves investigation, not excuses.

Tips: Test each protein in the final process, not only in a small beaker. Measure water absorption, viscosity, flavor, and texture over time. Keep batch records and compare supplier specifications carefully. Start with modest inclusion levels, then adjust gradually. Do not assume a familiar ingredient will behave identically across seasons. Manufacturers should also explain processing limits honestly to technical teams and customers. Cleaner labels can be valuable, but they do not automatically create better products.

What Challenges Do Manufacturers Face With Plant Proteins?

Plant proteins are nutrient-rich ingredients derived from crops such as soybeans, legumes, and peas. Their protein density varies considerably in their commonly consumed forms, affecting concentration, drying, formulation, texture, and processing efficiency.

Protein values are approximate grams per 100 grams of prepared food, based on USDA FoodData Central reference data. Lower protein density generally means manufacturers must remove more water or add more raw material to achieve a high-protein formulation.

Sourcing and Processing Challenges for Plant-Based Ingredients

Manufacturers face a sourcing problem before processing even begins. Protein crops vary by region, season, soil, and storage conditions. A pea shipment may show different protein levels, color, or flavor from the previous lot.

The Food and Agriculture Organization reports that agriculture uses about 70% of global freshwater withdrawals, so water availability can affect long-term crop planning. Drought adds another layer of uncertainty. It also exposes a weak assumption: plant protein is not automatically low-impact at every location.

Supply is often concentrated. This creates price pressure and makes traceability difficult. The Good Food Institute reported that global retail sales of plant-based meat reached approximately US$7.9 billion in 2023. That scale requires reliable, food-grade ingredients, not occasional surplus crops.

Manufacturers must verify origin, pesticide compliance, allergen controls, storage temperature, and microbial quality. One missed specification can alter an entire formulation.

Processing brings different obstacles. Dry fractionation can reduce water use, but it may produce lower protein purity. Wet extraction can improve functionality, yet it needs more water and energy. Heat treatment may reduce undesirable flavors and antinutritional factors, but excessive heat can damage solubility.

Texture is harder still. Protein particles can feel gritty, chalky, or dry. Small changes in milling size matter. Manufacturers often blend ingredients, adjust moisture, and test batches repeatedly. This is expensive. It is also where published data can feel incomplete, because laboratory performance rarely matches a full production line.

Managing Taste, Texture, Nutrition, and Product Consistency

Manufacturers face a practical taste problem: consumers compare plant proteins with familiar meat, milk, and eggs.

The Good Food Institute reported that U.S. plant-based meat retail sales reached about $2.2 billion in 2023, while unit sales declined roughly 13%. That gap suggests price matters, but sensory performance matters more. A dry patty, chalky shake, or beany aftertaste can quickly erase repeat purchases. Manufacturers often adjust protein blends, hydration, salt, fat, and cooking temperature. Small changes can affect firmness and juiciness.

Texture remains difficult.

Pea, soy, wheat, and fava proteins absorb water differently. Their particle size also changes bite and processing behavior. Nutrition adds another constraint. Processing may improve texture but increase sodium, while isolated proteins can require careful amino-acid balancing. The USDA FoodData Central database shows that protein values vary considerably among plant ingredients, so broad “high-protein” claims need verification. Consistency is equally demanding. Harvest conditions, moisture, and supplier batches can shift color, flavor, and viscosity. The 2023 GFI market data indicates strong consumer interest, yet declining unit sales warn manufacturers not to rely on novelty. In practice, tighter incoming-material testing and pilot-scale trials are essential. Even then, one formulation may perform differently after transport or extended shelf storage. That uncomfortable uncertainty deserves more attention.

Addressing Costs, Supply Chains, Regulations, and Sustainability

Manufacturers of plant-based proteins face pressure from several directions. The challenge starts with cost. Pea, soy, oat, and other protein inputs can fluctuate after poor harvests or transport delays. Processing also demands specialized equipment, careful temperature control, and skilled operators. A lower purchase price may still create higher costs through waste, rework, or inconsistent texture. That lesson is easy to miss.

Supply chains need flexibility. Factories often depend on limited growing regions, overseas shipments, or suppliers with seasonal capacity. A delayed shipment can leave workers waiting and production schedules under strain. Regional sourcing can shorten transit distances, but local supply may not meet volume or quality requirements. I have found that dual sourcing improves resilience, although it adds audits, contracts, and testing. It is not cheap.

Regulatory work requires accurate labels, traceable ingredients, and evidence for nutrition or environmental claims. Requirements differ across markets, complicating one formula or package. Sustainability adds another layer. Water use, land impact, energy consumption, and packaging should be measured across the product’s life cycle. Yet measurements are often incomplete. Manufacturers may report a smaller footprint while overlooking imported feedstock or processing energy. Transparent data, supplier checks, and realistic targets build credibility better than polished promises. The hard part is admitting what remains unknown.

Improving Manufacturing Technologies and Market Adaptation

Plant-protein manufacturers must improve processing while responding to changing consumer expectations. In pilot-scale trials, consistency is often harder than formulation. Small changes matter. Protein source, moisture, particle size, and mixing speed can alter texture. During extrusion, temperature and shear determine whether a product feels tender, fibrous, or rubbery. A few minutes of overheating may create a dry bite and a noticeable aftertaste.

Modern facilities need tighter process control and practical quality checks. Near-infrared testing can monitor moisture and protein levels during production. Digital sensors can track pressure, temperature, and residence time. However, equipment upgrades alone cannot solve every problem. Operators still need training, clear sampling procedures, and reliable supplier data. Cleaning systems also require attention because plant proteins can leave dense residues in pipes and mixing vessels. Wastewater treatment may become more demanding than expected.

Market adaptation requires more than copying animal-based textures. Consumers in different regions may prefer softer products, stronger seasoning, or simpler ingredient lists. Manufacturers should test prototypes with local users before expanding production. Small regional batches can reveal problems that laboratory panels miss. Cost remains a difficult issue, especially when specialized ingredients and energy-intensive processing raise prices. We sometimes assume consumers will accept higher costs for sustainability, but that assumption needs evidence. Better technology may reduce waste, yet imperfect batches still occur when raw materials change with harvest conditions. Firms should document these variations instead of hiding them, then adjust formulations and production settings with measurable criteria.

What Challenges Do Manufacturers Face With Plant Proteins? – Improving Manufacturing Technologies and Market Adaptation
Challenge Area Relevant Data or Benchmark Manufacturing Effect Technology or Process Response Market Adaptation Measure Priority Evidence Basis
Protein concentration Soy protein concentrates commonly contain at least 65% protein on a dry basis, while soy protein isolates commonly contain at least 90%. Pea concentrates and isolates vary substantially by raw material and process. Lower protein ingredients increase formulation volume and may affect nutrition claims, texture, and cost per serving. Use air classification, wet fractionation, membrane separation, and controlled drying to improve protein recovery and purity. Match protein concentration to the product category instead of using isolate-grade ingredients in every application. High Codex and food-protein ingredient specifications; peer-reviewed plant-protein processing literature.
Solubility and dispersion Plant proteins often show reduced solubility near their isoelectric point, typically around pH 4–5 for many legume proteins. Increased sedimentation, chalkiness, phase separation, and instability in beverages and liquid foods. Optimize pH, ionic strength, homogenization pressure, heat treatment, and protein pre-treatment; use enzymatic hydrolysis when appropriate. Develop separate formulations for neutral-pH beverages, acidic beverages, sauces, and high-protein nutrition products. High Food chemistry research on legume-protein solubility and functional properties.
Off-flavors Common sensory concerns include grassy, beany, bitter, earthy, and oxidized notes, particularly in some legume and oilseed proteins. Flavor masking can raise formulation complexity and may limit repeat purchase, especially in minimally flavored products. Apply rapid dehulling, blanching, controlled fermentation, aqueous washing, deodorization, and oxidation control. Use familiar flavor profiles, transparent ingredient communication, and consumer testing by region and age group. High Peer-reviewed sensory studies and reviews of plant-protein flavor formation.
Texture and fibrous structure Low-moisture extrusion is commonly operated at approximately 15–30% moisture, while high-moisture extrusion can operate at roughly 40–70% moisture, depending on formulation and equipment. Products may become too dense, rubbery, dry, soft, or inconsistent between production runs. Control feed moisture, screw configuration, shear, die temperature, cooling rate, and post-extrusion hydration. Offer texture formats suited to local eating habits, such as mince, strips, chunks, fillings, or ready-to-eat formats. High Published extrusion-processing studies and established process ranges reported in technical literature.
Heat sensitivity and processing loss Many plant proteins are processed under elevated temperatures; excessive heat can promote aggregation, reduce solubility, and intensify color or flavor changes. Lower functional performance, higher energy use, and inconsistent quality after drying, extrusion, or sterilization. Use temperature-time optimization, moisture control, staged heating, rapid cooling, and in-line monitoring. Prioritize processing conditions that preserve both protein functionality and the desired clean-label positioning. High Food engineering and protein-denaturation research.
Amino-acid balance Legume proteins are often relatively limited in sulfur-containing amino acids, while many cereal proteins are relatively limited in lysine. Single-source formulations may have a less balanced essential-amino-acid profile than animal-protein references. Blend complementary sources, such as legumes and cereals, and validate the final amino-acid profile analytically. Communicate protein quality using substantiated nutrition information rather than relying only on total protein grams. Medium FAO protein-quality guidance and amino-acid composition databases.
Digestibility and antinutritional factors Raw legumes can contain compounds such as phytic acid, trypsin inhibitors, tannins, and oligosaccharides; levels vary with crop, cultivar, and processing. Potential effects on digestibility, mineral absorption, flavor, and gastrointestinal tolerance. Use soaking, dehulling, germination, fermentation, extrusion, thermal treatment, and validated ingredient specifications. Provide clear preparation instructions and avoid unsupported digestibility or health claims. Medium FAO and peer-reviewed research on legume composition and processing.
Water and energy demand Wet fractionation requires substantial water handling, while drying and extrusion are energy-intensive unit operations; actual demand varies by process configuration and yield. Higher operating costs, wastewater treatment requirements, and environmental-footprint concerns. Improve solids recovery, recycle process water where permitted, use heat recovery, and select energy-efficient drying systems. Measure product-level environmental impacts using life-cycle assessment rather than broad ingredient assumptions. High Life-cycle assessment studies and food-process engineering analyses.
Raw-material variability Protein content and functionality vary with species, cultivar, growing conditions, harvest year, storage, particle size, and milling conditions. Variation in hydration, viscosity, extrusion behavior, color, flavor, and finished-product yield. Introduce supplier specifications, near-infrared screening, lot blending, standardized milling, and statistical process control. Design formulations with tolerance ranges and maintain alternative approved raw-material sources. High Grain and pulse quality research; industrial quality-control practice.
Allergen and labeling management Soy, wheat, and some other plant-derived ingredients may require allergen declaration depending on jurisdiction; regulatory requirements differ by market. Cross-contact risk, additional cleaning validation, label revisions, and restricted market access. Use dedicated lines where justified, validated cleaning procedures, segregation, traceability, and routine allergen testing. Review claims and declarations against the regulations of each target market before commercialization. High Applicable food-allergen and labeling regulations, including Codex principles and national requirements.
Cost competitiveness Total cost is influenced by crop price, protein yield, fractionation losses, energy, water, drying, packaging, and cold-chain requirements. High-purity ingredients and complex processing can raise retail prices above consumer expectations. Improve yield, use co-products, simplify formulations, localize supply, and optimize production scale. Target formats where convenience, nutrition, or sustainability provides value beyond price parity. High Cost drivers documented in plant-protein fractionation and food-manufacturing studies.
Consumer acceptance Acceptance is strongly affected by taste, texture, price, familiarity, preparation convenience, nutrition perception, and cultural food preferences. Technically successful products may still experience low repeat purchase if sensory performance or usage occasions are unclear. Use iterative sensory testing, rapid prototyping, texture measurement, and product-specific reformulation. Position products around familiar meals, convenient preparation, credible nutrition, and locally relevant flavors. High Consumer research and sensory-science literature on plant-based foods.
Shelf life and oxidation Residual lipids, oxygen exposure, moisture migration, and storage temperature can affect flavor and physical stability. Rancidity, color change, loss of crispness, caking, or separation during distribution and storage. Control water activity, oxygen exposure, particle size, packaging barrier properties, and storage conditions. Set shelf-life claims using real-time and accelerated stability testing for the finished product. Medium Food lipid-oxidation, packaging, and shelf-life research.
Scale-up and process integration Laboratory performance does not always transfer directly to pilot or commercial scale because residence time, heat transfer, shear, and mixing conditions change. Unexpected yield loss, texture variation, increased downtime, and difficulty meeting production targets. Use pilot-scale validation, digital process monitoring, design-of-experiments methods, and clearly defined critical process parameters. Launch in controlled product categories first, then expand after quality and supply reliability are demonstrated. High Food-process scale-up methodology and industrial extrusion research.
Data note: Values shown as ranges or benchmarks are indicative and can vary by crop, cultivar, ingredient specification, equipment, and regulatory jurisdiction. Protein percentages are generally reported on a dry basis unless otherwise stated.

FAQS

What are plant proteins?

Plant proteins are concentrated nutrients from peas, soy, lentils, beans, and grains. They can support muscle nutrition and reduce dependence on animal ingredients. Their functions also include binding, moisture retention, emulsification, and texture building.

Why do plant proteins behave inconsistently during manufacturing?

Harvest conditions, processing methods, storage time, moisture, and particle size can change protein performance. A powder may mix smoothly in a beaker but form stubborn lumps on a production line. Familiar ingredients may still behave differently across seasons.

How can manufacturers reduce earthy or beany flavors?

They can adjust protein blends, hydration, salt, fat, and cooking temperature. Sensory testing should examine aftertaste, dryness, and chalkiness after processing. Some flavor problems remain difficult.

What causes weak texture in plant-protein foods?

Different proteins absorb water differently and create different levels of firmness. During extrusion, temperature and shear influence whether the bite becomes tender, fibrous, or rubbery. A few minutes of overheating can produce dryness.

How should manufacturers test a new plant-protein formulation?

Test it in the final production process, not only in a small laboratory container. Measure water absorption, viscosity, flavor, and texture over time. Record batch conditions carefully. Early success may not last.

How does nutrition affect formulation decisions?

Protein values vary among plant ingredients, so high-protein claims require verification. Isolated proteins may also need careful amino-acid balancing. Improving texture can sometimes increase sodium or other formulation trade-offs.

Which process controls can improve consistency?

Digital sensors can track pressure, temperature, and residence time during production. Near-infrared testing can monitor moisture and protein levels. Operators still need training, sampling procedures, and dependable supplier records. Equipment alone is not enough.

What market factors should manufacturers consider?

Consumers may prefer softer textures, stronger seasoning, or simpler ingredient lists in different regions. Local pilot batches can reveal problems that laboratory panels miss. Higher prices may reduce repeat purchases, so sustainability assumptions need real evidence. Mistakes still happen.

Conclusion

Plant proteins are becoming increasingly important in modern manufacturing as producers seek more sustainable and flexible alternatives to animal-derived ingredients. However, what challenges do manufacturers face when using vegetal proteins? Key difficulties include sourcing reliable raw materials, managing seasonal variation, and developing efficient processing methods. Different plant sources can also produce noticeable differences in flavor, color, aroma, and functional performance, making it difficult to achieve stable product quality.

Manufacturers must balance taste, texture, nutrition, shelf life, and consistency while controlling production costs and maintaining dependable supply chains. They also need to meet changing regulatory requirements, communicate product qualities clearly, and reduce environmental impacts across processing and transportation. Advancements in extraction, blending, fermentation, and formulation technologies can help improve functionality and consumer acceptance. At the same time, manufacturers must remain responsive to changing market preferences by creating products that are practical, appealing, nutritious, and suitable for large-scale production.

Liam

Liam

Liam is a dedicated marketing professional with a profound expertise in the industry, where he excels at highlighting the unique advantages of our core products. With a keen understanding of market trends and consumer needs, Liam frequently updates our company’s professional blog, providing......