Featured High-Performance Protein Product Matrix
Explore our premium selection of engineered plant proteins, raw functional ingredients, and certified organic extracts designed for global nutrition leaders.
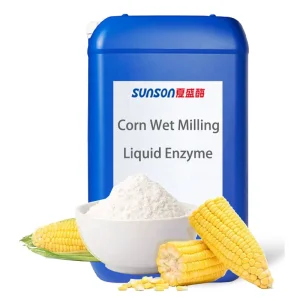
Corn Wet Milling Corn Separation Enzyme For Starch Production To Increase Maize Starch Yield
View Product
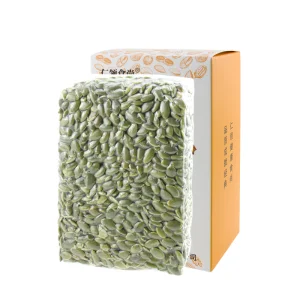
Pumpkin Seed Kernels - Original Flavor - Top-grade Baking Raw Material - Professional Export
View Product
Corporate Profile & Enterprise Competence
Dongguan Tsrel Biology Co., Ltd. represents the peak of modern vegetal protein engineering, offering world-class research, development, and scalable production.
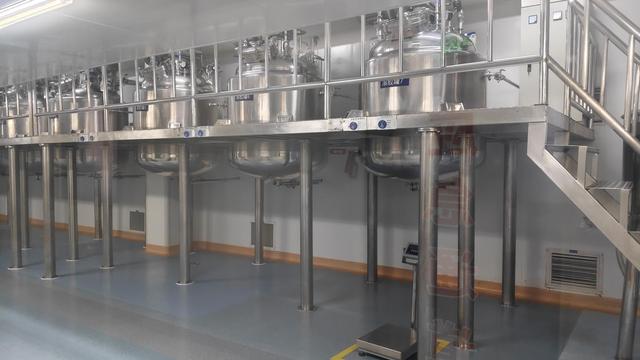
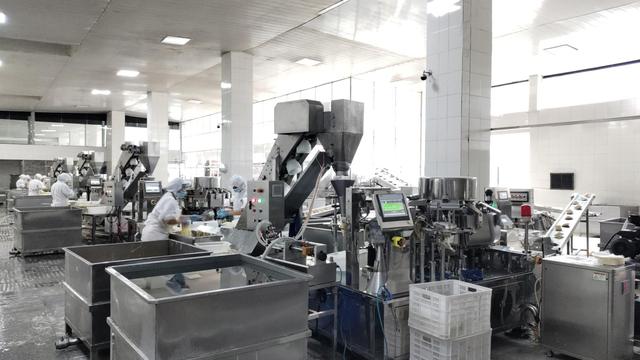
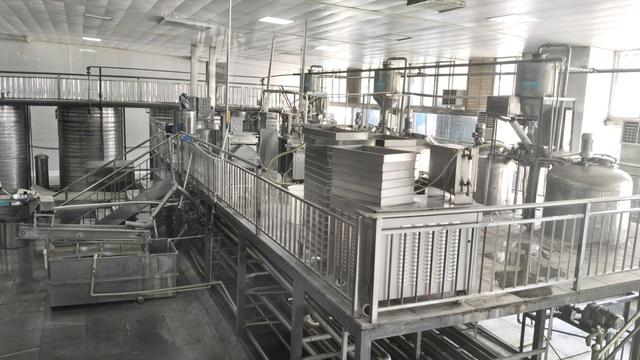
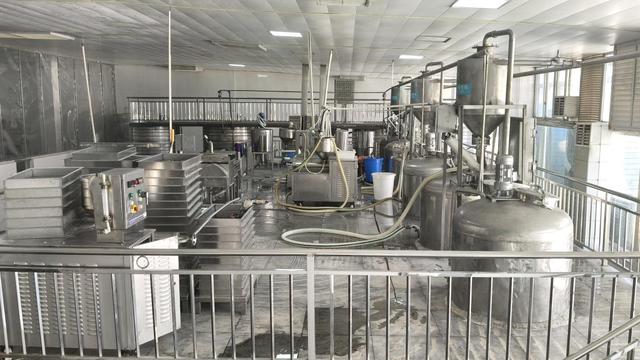
Dongguan Tsrel Biology Co., Ltd. is a professional China vegetal protein manufacturer specializing in the research, development, production, and supply of high-quality plant protein ingredients for food, beverage, and nutritional applications. With a strong focus on innovation, sustainability, and quality assurance, the company is dedicated to providing reliable plant-based ingredient solutions to customers worldwide.
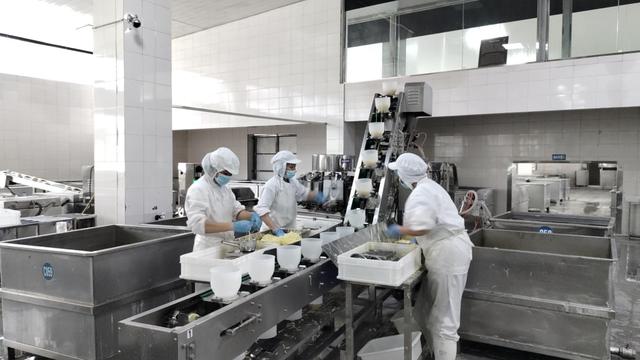
Equipped with advanced manufacturing facilities and modern processing technologies, Dongguan Tsrel Biology offers a comprehensive range of vegetal proteins, including soy protein, pea protein, rice protein, wheat protein, and other specialty plant proteins. These ingredients are widely used in functional foods, nutritional supplements, sports nutrition products, dairy alternatives, meat alternatives, beverages, bakery products, and health food applications.
Innovation is a key driving force behind the company's growth. Supported by an experienced research and development team, Dongguan Tsrel Biology continuously explores new technologies and application solutions to meet the evolving demands of the global food and nutrition industries. The company also provides customized ingredient solutions to help customers optimize product formulations, improve nutritional profiles, enhance texture, and create clean-label products.
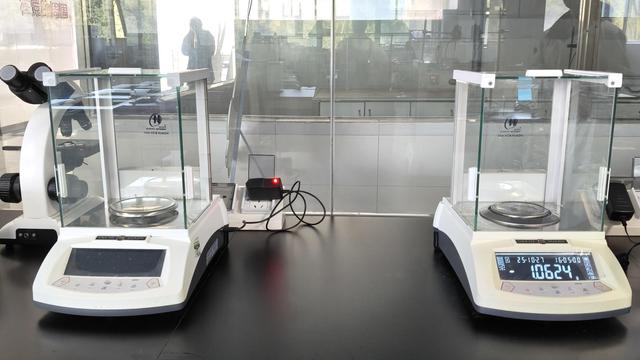
Quality and food safety are integrated into every stage of production. From raw material sourcing and processing to final testing and packaging, strict quality control procedures are implemented to ensure product consistency, purity, safety, and compliance with international standards. This commitment enables the company to deliver dependable products that meet the rigorous requirements of global customers.
With customer satisfaction at the center of its operations, competitive manufacturing capabilities, stable supply chains, and professional technical support, Dongguan Tsrel Biology Co., Ltd. has established long-term partnerships with food manufacturers, distributors, and brand owners across international markets. The company remains committed to advancing sustainable nutrition through innovative plant protein solutions for the global marketplace.
Macro Industry Solutions & Global Commercial Landscape
Analyzing the paradigm shift toward plant-based proteins, macro-economic drivers, and industrial integration standards worldwide.
Global Dietary Transition
The global food industry is undergoing a structural transformation driven by consumer demand for sustainable, hypoallergenic, and clean-label nutrient sources. Industrial manufacturers are rapidly reformulating traditional product portfolios to integrate high-purity plant proteins.
Supply Chain Resilience
Maintaining uninterrupted production cycles requires diversified agricultural sourcing and advanced extraction technologies. Our vertically integrated manufacturing model ensures absolute traceability from raw harvest to final bulk export container.
B2B Custom Formulation
Industrial clients demand customized functional parameters such as specific solubility indices, gelation properties, and neutral taste profiles. Our R&D application labs deliver bespoke formulations tailored precisely to target product specifications.
Compliance Assurance & Localized Global Support
Meeting stringent international regulatory frameworks through comprehensive certifications, rigorous quality audits, and localized technical services.
Navigating global regulatory compliance is paramount for international food and supplement brands. Dongguan Tsrel Biology operates under strict quality management systems aligned with global benchmarks, including ISO, HACCP, GMP, HALAL, and Kosher certifications. Every batch undergoes rigorous microbiological, heavy metal, and nutritional assay testing prior to dispatch, ensuring absolute safety and regulatory clearance across North American, European, and Asia-Pacific jurisdictions.
Furthermore, our dedicated technical support teams offer localized documentation, regulatory filing assistance, and formulation consulting. By bridging the gap between advanced manufacturing capabilities in China and regional compliance requirements abroad, we empower our global partners to accelerate time-to-market while mitigating operational risks.
Localized Application Scenarios & Industrial Integration
Discover how our specialized plant proteins enhance diverse product categories across commercial sectors worldwide.
Sports Nutrition & RTD Beverages
Engineered for high solubility and smooth mouthfeel, our protein isolates integrate seamlessly into ready-to-drink shakes, protein bars, and recovery powders without chalky aftertaste or sedimentation issues.
Plant-Based Meat & Dairy Alternatives
Providing excellent water-binding capacity, emulsification, and fibrous texture simulation, our functional proteins help manufacturers replicate the authentic bite and nutritional profile of animal-based analogs.
Bakery & Functional Confectionery
Upgrading traditional baked goods with clean-label protein enrichment, our ingredients improve nutritional density while maintaining structural integrity, crumb softness, and extended shelf life.
Technology Roadmap & Future Horizons
Pioneering the next generation of enzymatic hydrolysis, fermentation-derived proteins, and eco-friendly processing technologies.
Our long-term technology roadmap focuses heavily on advanced bioprocessing, enzymatic modification, and precision fermentation. By optimizing protein extraction efficiencies and minimizing water and energy consumption, we are continuously driving sustainable manufacturing innovations.
Future developments include micro-encapsulation technologies for enhanced nutrient delivery, customized peptide profiling for targeted health benefits, and fully circular agricultural waste valorization. These initiatives reaffirm our commitment to leading the global plant-based revolution through scientific rigor and environmental stewardship.
Frequently Asked Questions (FAQ)
Expert answers regarding our manufacturing standards, custom OEM capabilities, and global logistical operations.
What are the minimum order quantities (MOQ) for custom OEM protein formulations?
Our standard MOQ for custom private label formulations typically starts at 500kg to 1,000kg per run, depending on specific ingredient complexity and packaging requirements. We work closely with emerging brands and established enterprises to provide scalable solutions.
How do you ensure allergen control and product purity in your facilities?
We operate dedicated processing lines with strict segregation protocols for major allergens such as soy, wheat, and peanuts. Comprehensive ELISA testing and rigorous sanitation validations are performed continuously to eliminate cross-contamination risks.
What international shipping and export documentation do you provide?
We provide full export documentation packages, including Certificates of Analysis (CoA), Health Certificates, Non-GMO Statements, Allergen Declarations, and certification paperwork (ISO, HACCP, Halal, Kosher) required for smooth customs clearance worldwide.
Can you provide tailored technical samples for R&D testing?
Yes, we routinely supply sample kits and pilot-scale quantities to food scientists and product developers globally to support benchtop testing and formulation optimization prior to commercial scaling.
Complete Product Portfolio & Industrial Supply Range
Browse our full inventory of specialty seeds, high-grade protein isolates, and functional enzyme additives for global distribution.